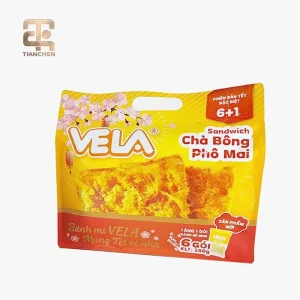
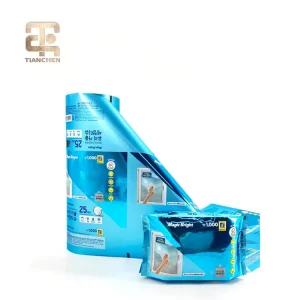
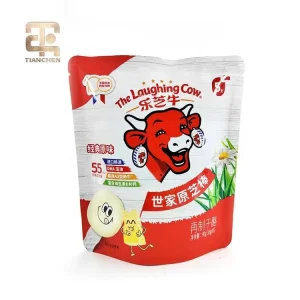
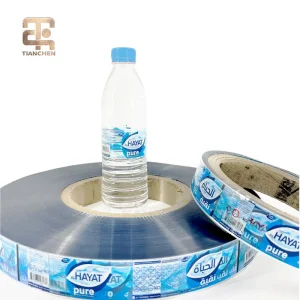
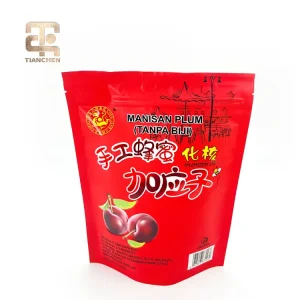
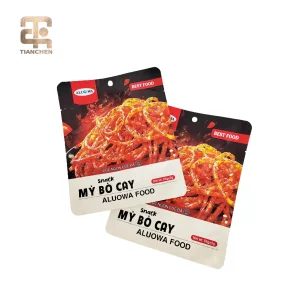
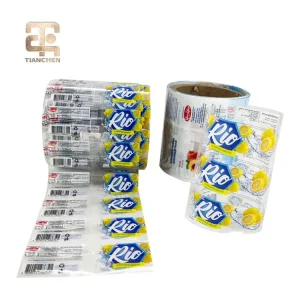
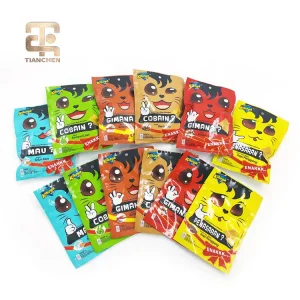
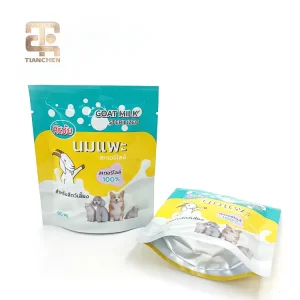
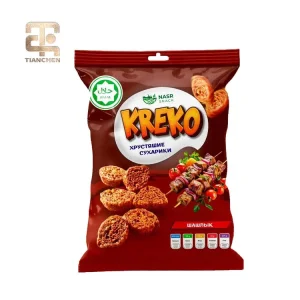
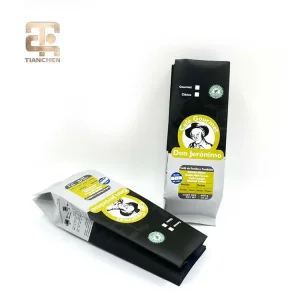
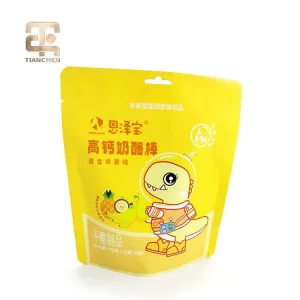
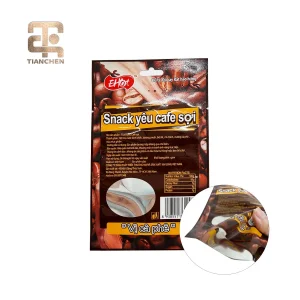
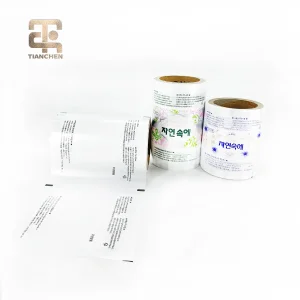
In the evolving landscape of global logistics, Bag-in-Box (BiB) technology represents a paradigm shift in efficient liquid and semi-liquid transportation. As a premier China supplier, we integrate barrier film innovation and ergonomic structural design to minimize environmental footprints while maximizing shelf-life extension.
Our manufacturing philosophy leverages Industry 4.0 standards, utilizing automated color matching, real-time quality inspection (AI-driven), and data-traceable production lines. This ensures that every batch meets rigorous international standards, providing our global clients with the supply chain reliability needed to navigate modern market volatility.
ISO9001, FDA, and BRC compliant facilities ensuring food safety.
Dedicated account managers providing 24/7 technical consultation.
Advancing towards 100% recyclable mono-material barrier structures.
Optimized logistics from Guangdong, the heart of Asian manufacturing.
Q: Why choose Chinese suppliers for Bag-in-Box solutions?
A: China offers unparalleled vertical integration, from resin production to high-speed automated printing, allowing for superior price-to-performance ratios.
Q: How do you guarantee quality?
A: We utilize smart monitoring systems for thermal stability and leak-proof testing, maintaining strict E-E-A-T compliance across all production cycles.
 TIANCHEN PRINTING